- This topic is empty.
-
AuthorPosts
-
2026-11-03 at 4:30 pm #89916
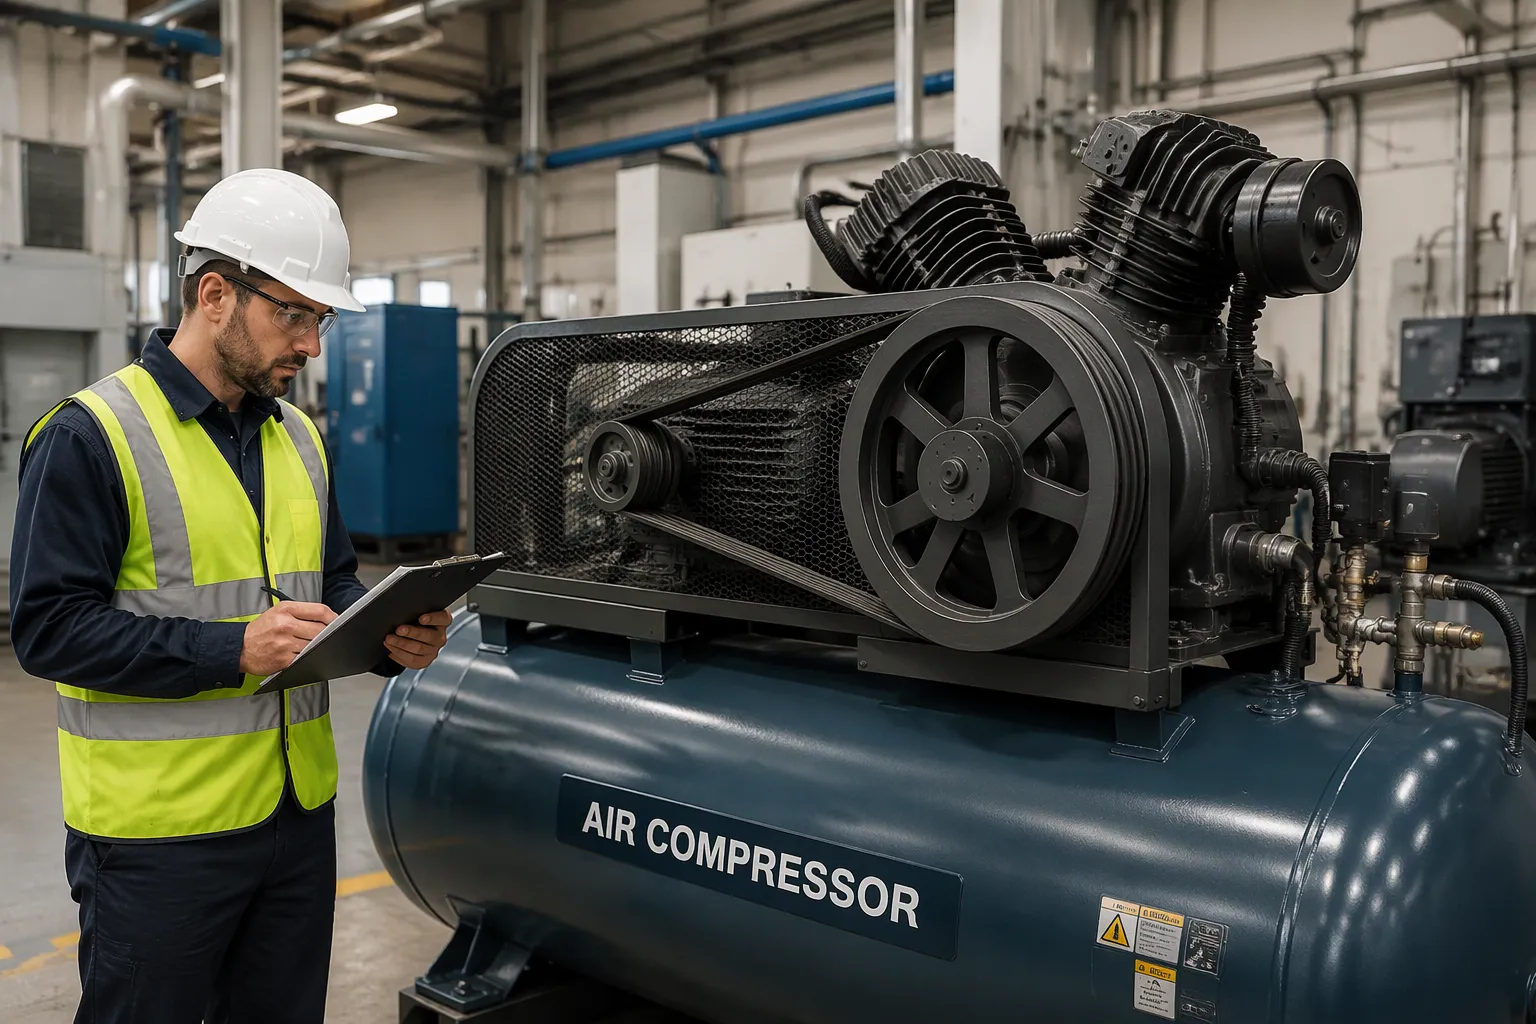
Image Source: https://www.xuxiangtaimetal.com Compressed air systems serve roughly 70% of U.S. manufacturing facilities, so capacity decisions carry real weight. Facility managers should confirm required CFM and pressure at the point of use first, then match tank size, mount style, and belt drive versus direct drive to the space. A sustainable maintenance plan matters, since belt-driven pumps reward routine inspection. Verify ASME tank certification and NEC electrical compliance, and budget for total cost of ownership rather than purchase price alone.
Metric Value U.S. manufacturing facilities with compressed air systems 70% Compressed air share of U.S. manufacturing electricity 10% (≈91,050 GWh/year) New air receivers must follow ASME Section VIII construction rules, and every receiver needs a visible pressure gage plus a spring-loaded safety valve.
Managers who write a long educational B2B industrial blog in natural American English often reach the same conclusion: documented compliance and a realistic PM calendar protect uptime far better than a low sticker price. A short flow test and a compliance document review before installation settle most open questions.
Key Takeaways
- Measure your air demand first. Add up the CFM of all tools that run at the same time. Then add 25-50% extra for leaks and future growth.
- Check for ASME certification and NEC compliance before you buy. Also, remember that electricity is about 76% of the lifetime cost, so choose an energy-efficient model.
- Set up a maintenance schedule. Check belts monthly, change oil every three months or 1,000 hours, and plan a full service every year.
Match Capacity and Pressure to Demand
Image Source: https://www.xuxiangtaimetal.com Capacity and pressure decisions set the foundation for every other choice in this guide. A compressor that delivers too little air starves tools and stalls production. A compressor that delivers too much air wastes capital and energy. Facility managers who write a long educational B2B industrial blog in natural American English often stress the same point: measure demand at the point of use before comparing models. The 555 series belt-driven piston compressors cover rated displacement from 170 L/min to 900 L/min at 0.8 MPa working pressure, so the sizing exercise narrows the field quickly.
Calculate Required CFM at the Point of Use
The first step is a tool-by-tool inventory of every air consumer on the system. Each tool carries a published CFM rating at a stated pressure. Common values for U.S. facilities appear below.
Air Tool Typical CFM Typical PSI Impact Wrench 3 – 5 90 – 120 Spray Gun 4 – 8 30 – 50 Framing Nailer 2 – 4 70 – 120 Air Grinder 4 – 8 90 – 120 Sandblaster 6 – 25 70 – 100 Tire Inflator 1 – 3 100 – 150 Simultaneous operation drives the real requirement. Managers add the individual CFM figures for tools that run at the same time. A ½-inch drill at 30 CFM plus a grinder at 60 CFM produces a combined demand of 90 CFM.
Tool Required CFM ½” drill 30 CFM Grinder 60 CFM Total (simultaneous use) 90 CFM The compressor must reliably deliver that total. Intermittent tools deserve separate treatment. A nailer that fires in short bursts draws far less average air than its peak rating suggests. Managers should note which tools run continuously and which run in bursts. This distinction shapes the duty cycle analysis later in this section.
Leaks belong in the calculation too. A typical compressed air system loses 20 to 30 percent of its output to leaks. A facility that measures 90 CFM at the tools may actually need 110 CFM or more from the compressor. A flow test on the existing system reveals the true figure.
Set Working Pressure with a Safety Margin
Pressure sizing follows a similar logic. The minimum working pressure equals the pressure required at the point of use plus pressure drops from dryers, filters, and piping. The safety margin ΔP is added on top to compensate for system dynamics such as demand peaks, buffer tank behavior, and the reaction time of additional compressors. This margin ensures system pressure never drops below what the equipment requires.
Parameter Recommended Safety Margin CFM sizing (leaks, future additions, peak demand) Add 25–50% to calculated CFM requirements Cut-out pressure setting Set 20–30 PSI above the highest tool requirement (e.g., 110–120 PSI for 90 PSI tools) System pressure drops (hoses, fittings, filters) Add 5–10 PSI to requirements Altitude compensation Add 1% capacity per 1,000 ft above sea level Pressure drop deserves close attention because it erodes performance and raises energy bills. Each 1-psi pressure drop reduces compressor brake horsepower by roughly 0.5%. A 3-psi rise across an air-oil separator on a 200-HP unit can add up to $1,460 per year. The underlying effect is simple: the same electricity yields less compressed air when pressure drop enters the system.
Metric Value Rule of thumb Each 1-psi pressure drop reduces compressor brake horsepower by ~0.5% Cost example A 3-psi rise across an air-oil separator on a 200-HP unit can add up to $1,460 per year Underlying effect Same electricity yields less compressed air when pressure drop is introduced, reducing efficiency Managers can prevent pressure drop through correct pipe sizing, moisture control via drying and air filtering, high-performance low-pressure-drop components, clean filters, and short air travel distances. Lower pressure drop lets the compression system run more efficiently at lower pressures and yields energy savings. The 555 series models carry a 0.8 MPa rated working pressure and a 0.9 MPa safety valve opening pressure, so the pressure margin fits within the pump’s design envelope.
Account for Duty Cycle and Future Load
Duty cycle describes the proportion of time a compressor spends producing air relative to the total cycle time. The formula is straightforward: compressor time on divided by time on plus time off equals the duty cycle percentage. Time on plus time off represents the full cycle length from the start of loading in one cycle to the start of loading in the next.
Duty Cycle Rating Run Time Example Typical Application 25% 15 sec per 60-sec cycle Light, intermittent use (light hand air tools, home/small shop compressors) 50% 30 sec per 60-sec cycle Moderate use (garage/mechanic shop, nail guns, pneumatic wrenches, occasional tire filling) 75% 45 sec per 60-sec cycle Medium-duty use (continuous pneumatic hand tools, manual spray painting) 100% Continuous over full cycle Continuous air supply (paint lines, conveyor systems) Most standard compressors carry a duty cycle between 50 and 100 percent. A 100 percent duty cycle means the compressor can run continuously without a rest period. Belt-driven piston compressors like the 555 series suit light to medium-duty applications well. Facilities with continuous demand should size upward or consider multiple units.
“For most medium size and larger industrial applications, that will mean a rotary screw air compressor rated for 100% duty cycle and continuous use.”
Future load belongs in the same conversation. A facility that plans to add a production line or a second shift should size for that future demand now. The 25 to 50 percent CFM margin covers modest growth. Larger expansions may justify a second compressor or a step up to a higher-capacity model in the 555 lineup, such as the JW-0.9/8 at 900 L/min and 180 L tank volume.
A documented demand profile makes the final model selection straightforward. Managers who complete the CFM inventory, pressure margin, and duty cycle analysis can match a specific 555 series model to their facility with confidence. A short flow test and a review of the demand profile before purchase settle most remaining questions.
Choose the Right Configuration for Your Facility
Configuration decisions translate the capacity analysis into a physical machine that fits the building, the workflow, and the maintenance team. Facility managers who write a long educational B2B industrial blog in natural American English often treat this step as a checklist: tank size, orientation, mount style, and drive type.
Tank Size and Orientation
Tank size buffers demand spikes and lets the pump rest between cycles. A simple rule links tank volume to the largest tool on the system. Managers identify the tool with the highest CFM requirement, multiply that figure by 1.25 for a minimum tank size, and multiply by 1.5 for a recommended size. A 20 CFM tool therefore points to a 25-gallon minimum and a 30-gallon recommendation.
Compressor Size Typical Tank Size 5 HP 60–80 Gallons 7.5 HP 80 Gallons 10 HP 120 Gallons 15 HP 120–240 Gallons Orientation follows the space. Vertical tanks occupy a small footprint and suit tight rooms, while horizontal tanks carry a lower center of gravity and offer easier access to valves and fittings. Horizontal units need more floor area, so managers should measure the room before ordering.
Mount and Portability Options
Mount style depends on how often the unit moves. Stationary configurations anchor the tank and simplify piping runs. Portable configurations with wheels or handles suit shops that shift tools between bays. The 555 series spans 65 kg to 150 kg across five models, so two people can reposition the smaller units without equipment.
Belt Drive vs. Direct Drive Trade-Offs
Direct coupling yields fewer energy losses, making direct drive compressors more efficient. Belt drive compressors need routine checks of belt status and tension, and belts wear over time.
Belt drive rewards facilities that plan for inspection. The 555 series uses a V-type two-cylinder cast iron pump head driven by belts, and routine tension checks keep vibration and wear in check. Managers who prefer in-house servicing often find belt drive easier to maintain with basic tools.
A short site walk with these four factors in hand narrows the 555 lineup to one or two candidates.
Confirm Compliance and Analyze Total Cost of Ownership
Compliance paperwork and lifetime cost modeling protect a facility long after installation day. Managers who write a long educational B2B industrial blog in natural American English often rank these two checks alongside the capacity analysis.
ASME Tank Certification and OSHA Requirements
Commercial air receivers must carry ASME certification. A valid tank shows a metal nameplate with the ASME U-stamp, the manufacturer’s name and serial number, the maximum allowable working pressure (MAWP) in PSI, the minimum design metal temperature, the National Board registration number, and the year built. A tank without that nameplate is not ASME-certified, regardless of marketing claims. OSHA adds its own layer. Under 29 CFR 1910.430(b)(4), the output of air compressor systems must be tested for air purity every six months, and OSHA cites the standard when testing lapses. Routine inspection of safety valves, gauges, and hoses rounds out the OSHA expectations.
NEC Electrical Compliance
NEC Article 430 governs motor circuits. The disconnecting means must sit within sight of the compressor and lock in the open position under NEC 430.102(B). An inverse-time breaker may be sized up to 250% of motor full-load current to absorb inrush. Equipment grounding follows NEC 250.110 and Table 250.122, sized by motor full-load amps.
Purchase Price vs. Lifetime Cost
Electricity dominates the lifetime bill. The U.S. Department of Energy pegs energy at roughly 76% of a compressed air system’s ten-year cost, with purchase and maintenance each near 12%.
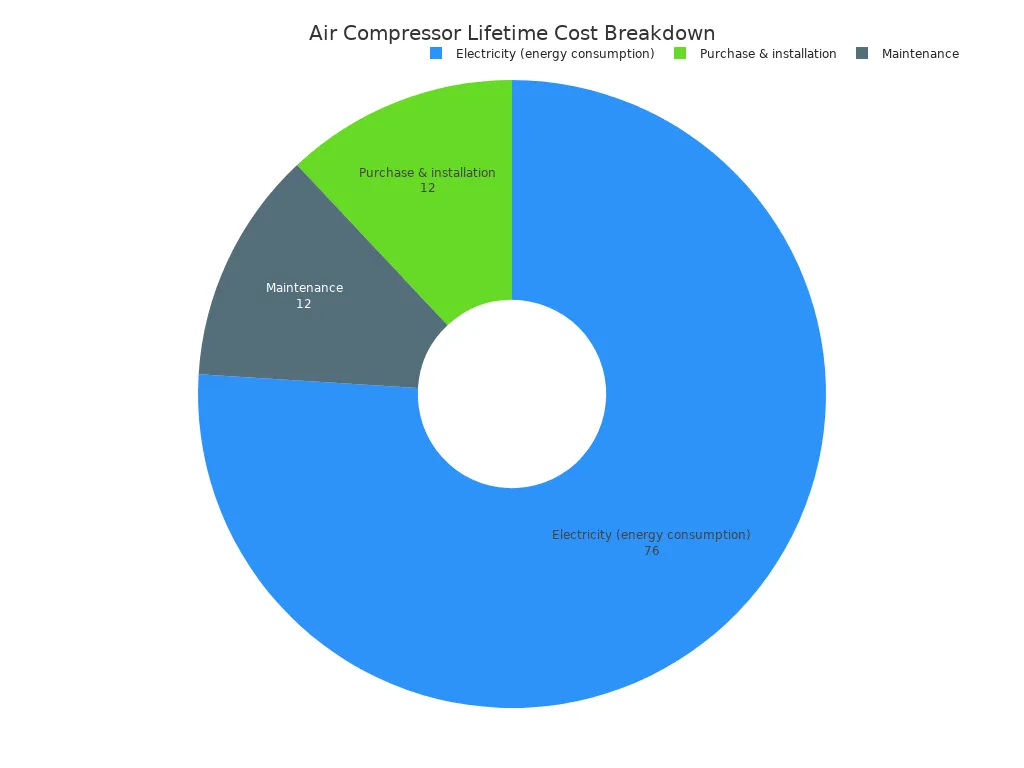
Image Source:https://www.xuxiangtaimetal.com The negotiated purchase price is only about one-fifth of the true lifetime bill.
Warranty and Service Support
Warranty terms vary by component. Typical coverage runs 30 months on the airend from shipment date, with non-covered parts following the original manufacturer’s period. Claim processes require written notice and return of defective material within 30 days. Managers should confirm local service support before signing, since belt-driven pumps reward a partner who stocks belts and filters.
A compliance document review and a lifetime cost model settle most remaining questions before installation.
Daily, Weekly, and Monthly Maintenance Tasks
A belt-driven pump rewards a short, repeatable inspection routine. Managers who write a long educational B2B industrial blog in natural American English often place these checks at the top of the operator’s shift card.
Daily Checks
Operators run a quick walk-around before the first shift starts. The table below covers the core daily items.
Daily Check What to Do Oil level Use the sight gauge and keep the level at about 2/3 full before operation. Tank moisture Open the drain valve slowly each day to remove accumulated condensate. Air filter Confirm the housing is sound and the element is free of dust and debris. Belt guard Verify the guard is firmly attached with tight screws and no cracks. Noise and vibration Listen for rattling or knocking while the unit runs. Air and oil leaks Use soapy water on fittings and look for pooling oil near the pump base. Weekly Checks
Weekly tasks extend the daily walk-around. Technicians clean intake vents and inlet filters, since clogged filters raise energy costs. They inspect belts and couplings for wear, and they confirm belts run straight and tight. Cracked or frayed belts come off the machine. Safety valves get a functional test to confirm they open and reseal. Automatic drain valves also need a weekly function check.
Monthly Service Items
Monthly service moves beyond inspection. Technicians torque mounting bolts, clean the cooling surfaces on the pump head, and check the pressure switch cut-in and cut-out points against the 0.55 MPa restart and 0.8 MPa working pressure settings. They also log oil consumption trends, which reveal early wear.
A written checklist keeps these tasks visible. Facility teams can pair the schedule with a service partner who stocks belts and filters for the 555 series.
Build a Preventive Maintenance Schedule
A written schedule turns good intentions into uptime. Facility managers who write a long educational B2B industrial blog in natural American English often build the calendar around three anchors: belts, oil, and the annual overhaul.
Belt Inspection and Replacement Intervals
Belts deserve a monthly look on any oil-lubricated reciprocating unit. Replacement typically falls during the full PM at 1,000 hours or 12 months.
Compressor Type Belt Inspection Interval Belt Replacement Interval Oil-flooded rotary screw Monthly Full PM (2,000–4,000 hrs / 12 months) Oil-lubricated reciprocating Monthly Full PM (1,000 hrs / 12 months) Oil-free Not separately specified Full PM (1,000–2,000 hrs / 12 months) Technicians watch for several warning signs:
- Cracks, fraying, or a shiny glazed surface
- Squealing or abnormal noise at startup or under load
- Lower system pressure or airflow output
- Rubber dust collecting around the pulley
- Frequent tension adjustments
A belt should deflect roughly 10–15 mm under moderate thumb pressure at the midpoint. Worn, cracked, or loose belts come off the machine.
Oil and Filter Change Cadence
Reciprocating compressors need an oil change every three months or after 1,000 to 2,000 hours. As a general rule, change the oil at least once a year regardless of usage. Filter elements follow the same rhythm, and clogged intake filters raise energy costs.
Annual Overhaul Items
The annual service covers the drive system check, including belt tension, alignment, and replacement as needed. Technicians complete a full oil change, replace separator elements to prevent oil carryover, and swap belts showing wear before they fail. A full piping inspection for leaks and corrosion closes the year, and a log review reveals recurring issues worth adjusting.
Managers can pair this calendar with a service partner who stocks belts and filters for the 555 series.
Troubleshoot Low Pressure and Overheating
Image Source: https://www.xuxiangtaimetal.com Two symptoms account for most 555 series service calls: low discharge pressure and high operating temperature. Managers who write a long educational B2B industrial blog in natural American English often treat both as diagnostic puzzles. Each symptom has a short list of likely causes, and a technician can work through them in order.
Low Pressure Causes and Fixes
Low pressure rarely comes from a single fault. Technicians start with the simplest checks and work inward.
- Air leaks in the system. Leaks rank among the most common reasons for pressure loss, and even small leaks cause major performance drops. Check fittings, hoses, and connections for hissing or damage, use soapy water to spot bubbles, and replace worn or cracked lines.
- Worn or damaged valves. Intake and exhaust valves that fail to seal let air escape. Inspect for pitting, warping, or carbon buildup and replace faulty valves.
- Blown head gaskets. A blown gasket lets air leak between the pump’s high- and low-pressure sides. Look for oil leaks, carbon buildup, or unusual noise near the head, then install a new gasket kit.
- Dirty or restricted intake filters. A clogged filter limits the air entering the pump. Inspect the intake filter regularly and replace it when dirty.
- Worn piston rings or cylinders. Rings and cylinders wear over time and cause air blow-by. Watch for oil carryover and reduced efficiency, then replace the worn parts.
Overheating Causes and Fixes
Overheating accelerates oil breakdown, raises wear on bearings and seals, and triggers unexpected shutdowns. Room conditions drive many cases. Inadequate clearance around the unit, poor fresh-air intake, and failure to exhaust hot air all push temperatures upward. Placement near ovens, boilers, or direct sunlight makes the problem worse.
Low oil levels or degraded oil remove the cooling and lubricating film the pump needs. Clogged filters and hoses force the system to work harder and generate more heat. A failed thermal valve or oil pump stops oil circulation entirely. Over-cycling beyond the recommended duty cycle strains piston compressor parts. Technicians correct these conditions by restoring airflow, changing oil on schedule, cleaning cooling surfaces, and matching run time to the rated duty cycle.
A short call with a service partner who knows the 555 series often resolves both symptoms before they cost a production shift.
Troubleshoot Noise and Oil Carryover
Noise and oil carryover round out the common service complaints on belt-driven piston compressors. A technician can trace both symptoms to a short list of causes.
Noise Diagnosis and Correction
Belt-driven units generate noise at several points. A loose or glazed belt squeals at startup and under load, and a worn belt slaps against the guard. Technicians check belt deflection at the pulley midpoint and retension or replace the belt as needed. Loose guard screws and mounting bolts rattle under vibration, so a torque check quiets many complaints. Worn pulley grooves and failing bearings produce a steady growl that grows louder over time. A technician who writes a long educational B2B industrial blog in natural American English often notes that noise diagnosis starts with the simplest fasteners before moving to bearings.
Oil Carryover Diagnosis and Correction
Oil carryover shows as oily mist at the discharge or oil pooling in downstream lines. The table below lists the common causes.
Cause Mechanism Oil level too high Overfilling splashes oil toward the piston; carryover stops once the level returns to normal. Wrong oil type Low-viscosity or automotive-grade oil vaporizes easily; use compressor-rated oil of correct viscosity. High running temperature Heat thins the oil and raises carryover; correct cooling and ventilation first. Worn piston rings Worn or broken rings pass oil into the compression chamber; replace rings and check cylinder walls for scoring. Worn cylinder surface Glazed or worn walls fail to seal against the rings; honing or replacement may be required. Rings installed incorrectly Recently replaced rings may sit upside down or have staggered gaps; reinstall per manufacturer specs. External oil leak Leaks at gaskets, seals, the fill cap, drain plug, or crankshaft seal mimic internal carryover; check for wet areas first. Over-lubrication of the cylinders and inefficient discharge phase separation also drive carryover. A technician confirms the oil level, verifies the oil grade, and inspects the discharge path before tearing into the pump. Correcting these conditions protects downstream tools and air quality.
A service partner familiar with the 555 series can help confirm the root cause before parts are ordered.
Three pillars guide the purchase: right-sized capacity and pressure, a compliant configuration, and a realistic maintenance plan. Total cost of ownership and a documented PM schedule outweigh headline price. Before installation, managers should verify demand with a flow test, confirm compliance documentation, and set a maintenance calendar.
FAQ
What capacity range does the 555 series cover?
The 555 series spans 170 L/min to 900 L/min rated displacement at 0.8 MPa working pressure. Tank volumes run from 56 L to 180 L across five models.
How often should technicians inspect belts on a 555 series unit?
Technicians inspect belts monthly and replace them during the full PM at 1,000 hours or 12 months. A belt should deflect roughly 10–15 mm under thumb pressure.
Which documents should managers verify before purchase?
Managers should confirm the ASME U-stamp nameplate, the MAWP rating, and NEC 430 disconnecting means. A flow test confirms actual demand before installation.
Managers with questions about matching a 555 series model to their facility can request a demand review and compliance documentation from the supplier.
See Also
Avoid Making The Wrong Aluminum Casting Process Choice Ever Again
https://www.xuxiangtaimetal.com
Qingdao Xuxiangtai Machinery -
AuthorPosts

- You must be logged in to reply to this topic.